Leveraging decades of manufacturing excellence, we provide the tallest tower cranes tailored to diverse international construction needs. Our deep understanding of global markets ensures each machine meets stringent quality and performance standards.
Explore Our Global PresenceOur factory is at the forefront of tower crane technology, integrating advanced materials, intelligent control systems, and enhanced safety features. We are committed to continuous research and development to offer the most efficient and reliable lifting solutions.
Discover Our Tech RoadmapWe embody Experience, Expertise, Authoritativeness, and Trustworthiness. Our long-standing history, industry-leading professionals, extensive certifications, and transparent practices guarantee the highest level of confidence for our clients worldwide.
Our Commitment to E-E-A-TOur tower cranes are engineered for versatility, empowering diverse construction projects across varied terrains and climates. From soaring skyscrapers to complex infrastructure, we provide the critical lifting power.
In densely populated urban centers, our tallest tower cranes enable the efficient construction of supertall skyscrapers, providing precise material handling at extreme heights and minimizing site footprint.
Inquire for High-Rises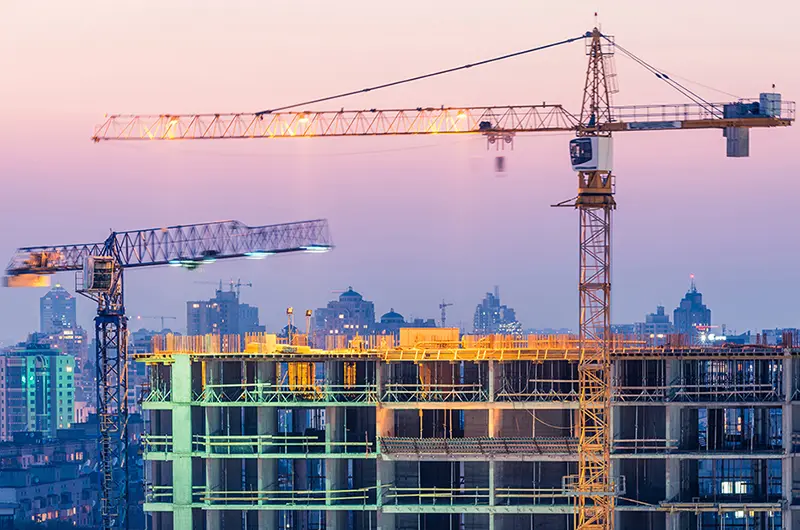
For bridges, airports, and industrial complexes, our robust tower cranes handle massive components, contributing to rapid project timelines and ensuring the structural integrity of critical public works.
Learn About Infrastructure Solutions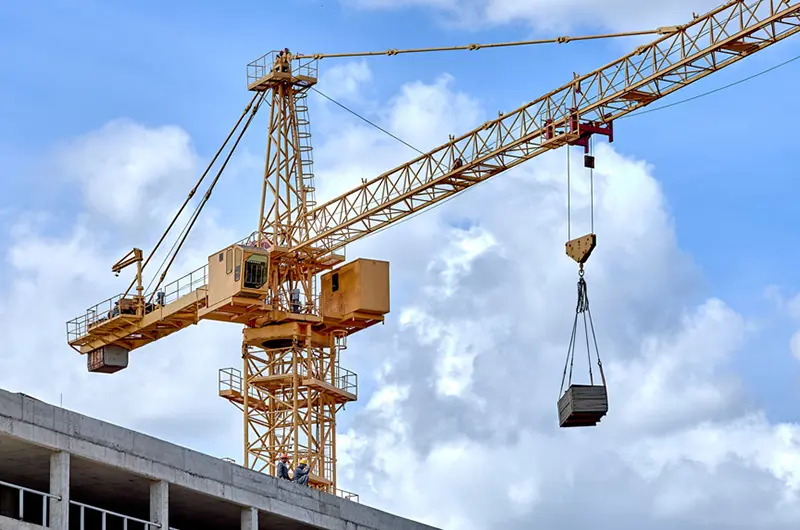
Engineered for extreme conditions, our tower cranes operate reliably in harsh environments, from arid deserts to icy terrains and high-wind regions, ensuring consistent productivity.
Explore Extreme Solutions
Our tallest tower cranes are integral to constructing power plants, refineries, and manufacturing facilities, handling heavy industrial equipment with precision and safety.
Discuss Industrial NeedsWe are dedicated to pioneering the future of vertical construction. Our R&D focuses on enhanced efficiency, automation, sustainability, and user safety.
Integration of IoT sensors for real-time data on performance, load monitoring, predictive maintenance, and remote diagnostics. AI-driven operational optimization for enhanced safety and efficiency.
Focus on developing energy-efficient crane designs and utilizing eco-friendly materials. Reducing the carbon footprint of manufacturing processes and optimizing crane lifecycle management.
Exploring automated assembly, remote operation capabilities, and robotic assistance for maintenance and inspection, further enhancing safety and productivity in complex site environments.
Developing modular crane components for easier transport, faster assembly, and enhanced adaptability to project-specific requirements and evolving site conditions.
Our strategic manufacturing base in China offers unparalleled advantages in supply chain resilience, cost-effectiveness, and rapid production capacity.
We maintain strong relationships with a vast network of raw material suppliers and component manufacturers, ensuring consistent availability and competitive pricing even during global disruptions.
Our state-of-the-art manufacturing facilities employ advanced production techniques and lean management principles, enabling high throughput and rapid turnaround times from order to shipment.
Quality assurance is integrated into every stage of production, from material inspection to final assembly and testing, ensuring that every crane leaving our factory meets international standards.
Understanding the diverse needs of the global construction market, we position our tallest tower cranes as critical assets for large-scale international projects.
As developing economies accelerate infrastructure development, the demand for high-capacity and tall tower cranes is surging. We provide reliable, cost-effective solutions to support this rapid growth.
In mature construction markets, the focus is on efficiency, safety, and complex urban projects. Our technologically advanced tower cranes meet these demands with features like advanced load control and remote monitoring.
The global construction industry is driven by urbanization, technological adoption, and sustainability goals. Our tallest tower cranes are designed to align with these trends, offering high-performance and eco-conscious solutions.
We ensure seamless integration of our tallest tower cranes into your projects through tailored support and rigorous adherence to international compliance standards.
Our expert team provides pre-sales consultation to help select the optimal tallest tower crane model for your specific project needs, including site analysis and load calculations.
All our tallest tower cranes are manufactured to meet or exceed stringent international safety and quality certifications (e.g., CE, ISO). We provide comprehensive documentation for smooth import and operation in any region.
Our experienced logistics team manages seamless transportation to your site. We also offer after-sales support, including spare parts and technical assistance, to ensure your crane's long-term performance.
We provide guidance and necessary documentation to facilitate customs clearance and ensure compliance with local regulations in your project's destination country.
Our "tallest" designation refers to our capability to engineer and manufacture tower cranes with exceptionally high hook heights and superior lifting capacities, suitable for supertall skyscraper projects and other extremely tall construction endeavors. This is achieved through advanced boom designs, powerful hoisting mechanisms, and robust mast section engineering.
E-E-A-T is built into our core operations: Experience: Decades of manufacturing and supplying tower cranes globally. Expertise: Our engineering and technical teams are industry leaders. Authoritativeness: We hold numerous patents and adhere to international standards, recognized by industry bodies. Trustworthiness: Transparent communication, verifiable certifications, robust quality control, and reliable after-sales support build lasting trust.
Our roadmap focuses on smart crane technology (IoT, AI), sustainable manufacturing with eco-friendly materials, enhanced automation for safety and efficiency, and modular designs for adaptability. We aim to lead in developing cranes that are not only powerful but also intelligent, sustainable, and user-friendly.
Our strategic location in China provides access to a highly resilient and efficient supply chain. This translates to competitive pricing, rapid production cycles, and a consistent supply of high-quality components and finished cranes, even amidst global market fluctuations. Our extensive network ensures reliability and cost-effectiveness.
We provide comprehensive documentation and certification to meet international standards (CE, ISO, etc.). Our team assists with understanding and navigating local customs regulations and operational requirements in your specific country, ensuring a smooth and compliant deployment of your tower crane.








